PCB Assembly, Aging Test and SMT Assembly: Four Sets of Figures for One Purchase
An industrial computing order is quoted, built and shipped, and then four people inside the same building are asked what it returned. The purchasing lead quotes a booked price. The production planner quotes hours per board. The quality engineer quotes a return count. The process engineer quotes the margin left in the profile. All four are answering honestly, and none of the four answers will reconcile with the others, because they are not describing the same quantity.
This is not a reporting failure that a better spreadsheet will fix. The four figures are computed against different denominators, on different clocks, and with different definitions of what counts as an outcome. The useful question is therefore not which figure is right, but which figure a given decision actually needs. The sections below separate the four ledgers, name what each one measures, and identify the entries that quietly move from one ledger to another.
Why the Same Board Lands in Four Ledgers
Take one batch of boards from an industrial pc solutions order. Purchasing records what was committed at the moment the order was placed. Production records the hours the line spent, divided by the number built. Quality records how many units came back from the field over the following year. Engineering records the width of the process window that was consumed to get the batch through, which is a figure that exists in no financial system at all. Each number is defensible in isolation. Put side by side they look contradictory, and the contradiction is structural rather than arithmetic.
| Function | What it counts | Denominator it uses | What it never sees |
|---|---|---|---|
| Purchasing | Committed spend at order | The order it placed | Anything changed after the order |
| Production | Line hours consumed | Units of that batch | Field returns, months later |
| Quality | Units returned or reworked | Units shipped in the period | Where the margin went |
| Process engineering | Window consumed | Not financial | Any entry in any ledger |
The Denominator Is the Batch You Actually Run
Hours per board is the figure that moves most, and it is usually read as an efficiency signal when it is nothing of the kind. Changeover, first-article verification and stencil setup are largely fixed per run. Divide that fixed block by two hundred boards and it dominates the result. Divide it by two thousand and it almost disappears. The same line, the same operators and the same equipment therefore produce two very different hour counts, and neither of them is a measure of how well the line performed.
This matters when a smaller follow-up order is priced against the record of a large first article. The comparison looks like a cost increase and is described as one, although nothing about the process changed. The defensible way to read the figure is alongside the batch size it was derived from, which is exactly the detail a summary table drops first.
What Procurement Books Before the Board Is Even Placed
Purchasing commits the largest single share of an industrial build at the point of order, and from that moment the number is fixed on paper. What is fixed, however, is a unit price, not the cost of the part as it will eventually ship. A revision to the artwork, a substitution on one passive component, or an extra verification pass after a first-article discrepancy all land outside the committed figure.
So when a purchasing summary is presented as the cost of an industrial computing board, it is really the cost of the board as specified on the day the order was placed. The gap between those two statements is what separates a useful quote review from a discussion about price alone, and it is why a disciplined PCB assembly programme keeps the change record beside the order record.
Reliability Testing Sits in a Different Ledger
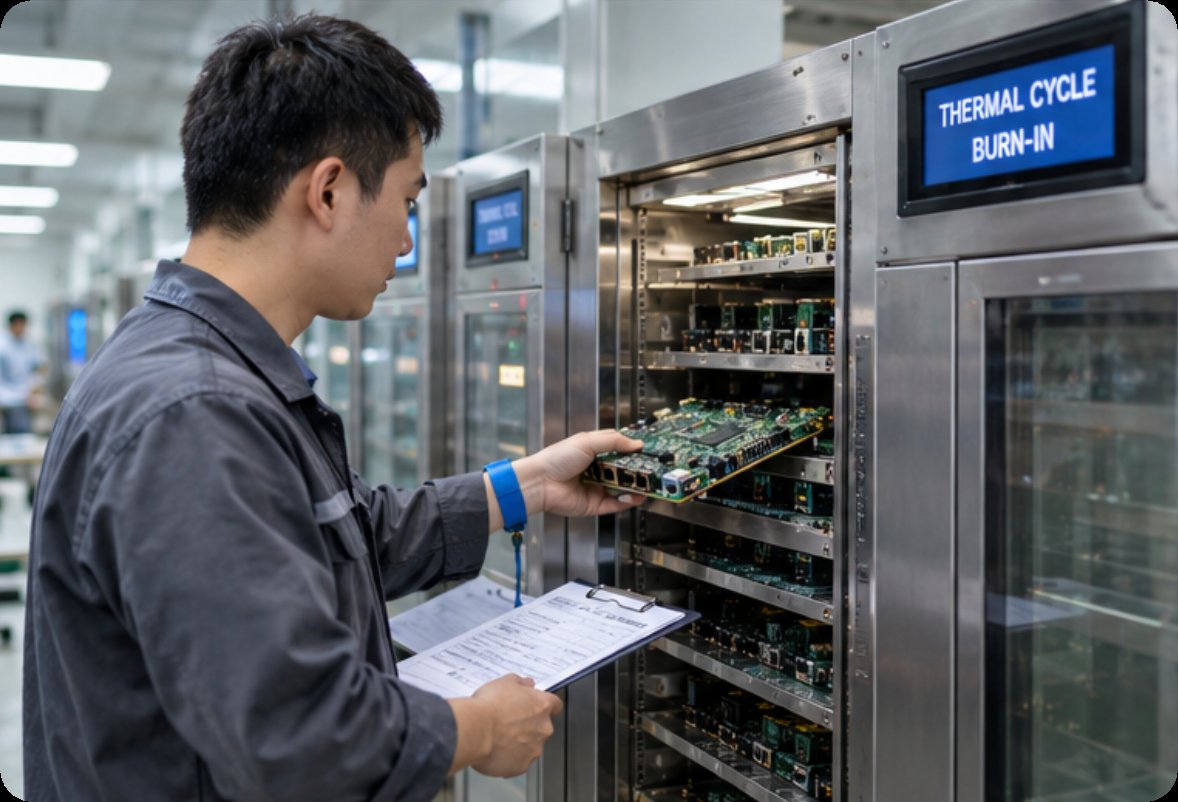
Reliability work is the clearest case of a return that arrives in the wrong ledger. A burn-in or thermal cycling programme consumes floor space, power and technician hours now, and returns its value months later as a lower field failure rate. On the day the cost is incurred it is an expense. On the day the benefit lands it appears as an absence of returns, a figure nobody is asked to explain and no cost centre can claim.
That asymmetry is why extended aging is often the first item cut when a schedule tightens. The cut is rational from any single ledger's point of view and expensive from the customer's. The practical remedy is to attach the programme to the failure modes it is meant to expose, so the spend is reviewed against something specific rather than defended as general prudence, and to treat an aging test as a defined intervention with a named target.
Process Margin Is Bought, Not Measured
Every build consumes process margin, and margin is acquired at the quotation stage rather than discovered on the line. Wider stencil apertures, a more generous thermal profile, tighter component tolerance classes, extra inspection and reflow profiling all widen the window a batch can survive. They are priced in before the first board is placed and invisible afterwards, because a process that ran comfortably and one that ran at its limit produce identical output.
The consequence is that two suppliers can quote the same operations and deliver very different durability of result, with no line item distinguishing them. Margin also has a shelf life: it is consumed by schedule pressure and by substitutions made after the order. A second build running the same profile as the first is not running with the same margin available, and the difference will only surface when something on the board changes.
Rework Appears in One Column Only
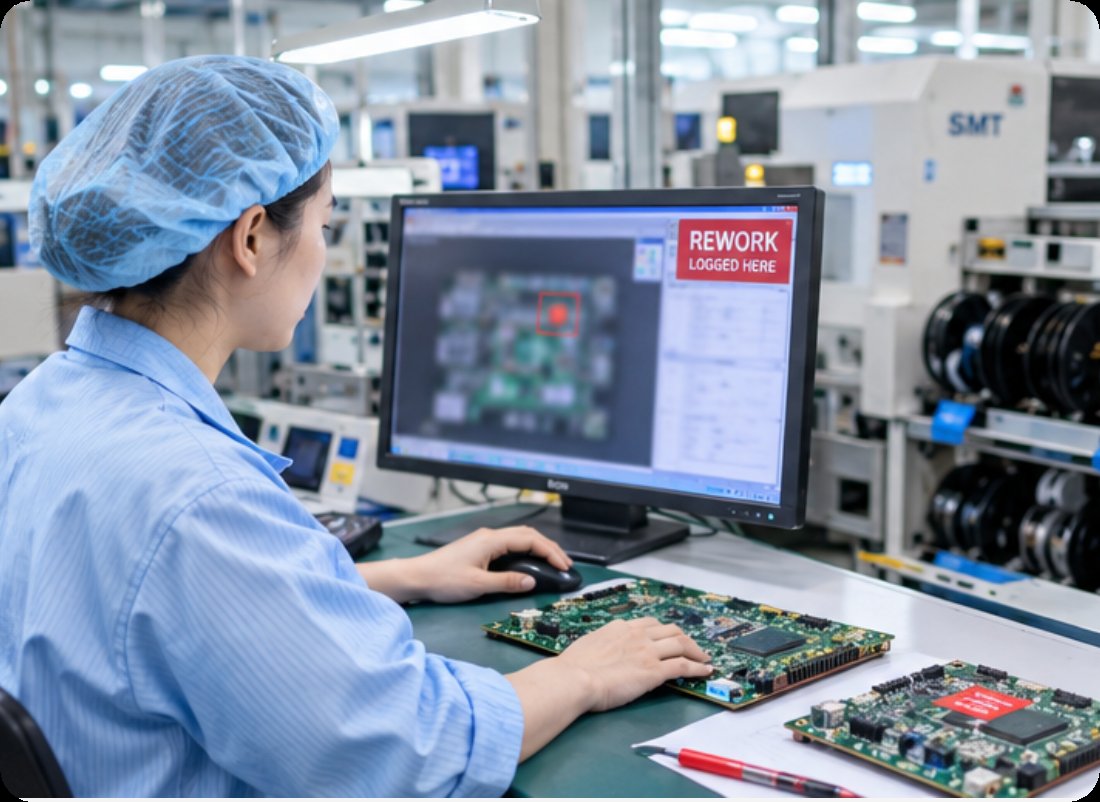
Rework migrates between ledgers most readily. To production, a unit corrected and shipped on time is a completed unit, and the hours spent on it vanish into the batch total. Quality records a defect that existed and was caught. Both are accurate, so one build can be recorded as fully delivered and as carrying a known defect rate at once.
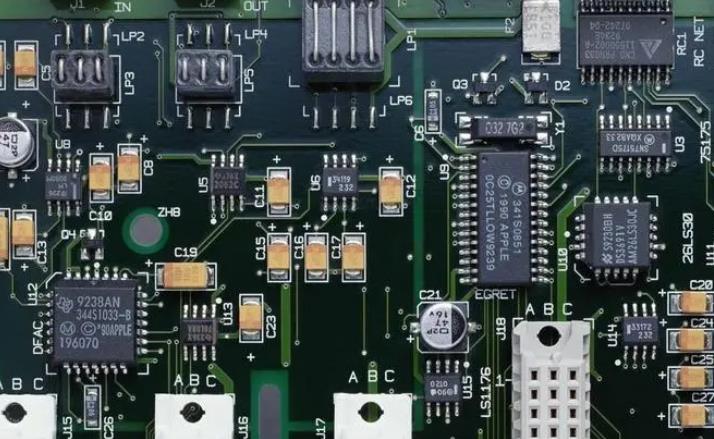
The crossover, where the two ledgers meet, is the only place the cost of a marginal process becomes legible. That shows most clearly in surface mount work, where a fine-pitch placement drifting slightly out of position is caught and corrected rather than scrapped, so the failure reaches no scrap figure and leaves the production total untouched. Reading SMT assembly performance without the rework column means reading only the half of the story that shipped on time.
Reconciling the Sheets Without Averaging Them
The instinct when four figures disagree is to average them, and averaging is the one action guaranteed to destroy all four. The figures have different denominators and different clocks, so their mean has no denominator and no clock at all. What actually works is a reconciliation in the literal sense: walk the same physical unit through all four ledgers and confirm that every cost it incurred was recorded exactly once, and that nothing was recorded in a ledger that cannot see it.
Two questions do most of the reconciling. Which entry was counted twice, and which entry was counted by nobody. Double counting is common where a correction is logged both as hours and as a quality event. Missing entries cluster around anything that has no natural home, which in practice means margin, test time and the engineering effort consumed by a change. Naming those gaps is more useful than closing them on paper.
| What is bought | Where the return lands | Who sees it first | Ledger that misses it |
|---|---|---|---|
| Assembly of a defined board | Units shipping to specification | Production | Purchasing |
| Reliability screening | Fewer field failures, later | Quality | Production |
| Placement capability | Fewer corrections per build | Quality | Purchasing |
| Process margin | Durability across revisions | Engineering | All financial ledgers |
The Sheet You Take Into the Next Review
Which of the four figures belongs in the next conversation depends on what is being decided. A sourcing decision needs the committed position plus a written account of what falls outside it. A scheduling decision needs hours expressed against the batch size they were divided by. A reliability decision needs the failure modes the programme is aimed at. A capability decision needs the margin level the work will run at, which is the hardest of the four to put on a page.
Bringing the wrong one is not a small error, because each sheet answers a question the others cannot. A supplier who can say which figure they are quoting, which entries sit outside it, and what would have to change for the number to move is describing a manufacturing process rather than a price. That conversation opens best by asking which ledger the other party is reading from, rather than by comparing totals never computed on the same basis. The suppliers who keep all four visible are usually the ones whose electronics manufacturing services hold up across a second and third build.
Tags: SMT assembly / industrial computing /
Prev: Custom Electronic Devices PCBA and DIP Assembly: The Lines the File Left Unwritten
Next: No more...