Aging Test, DIP Assembly and SMT Assembly: What the Line Maintains Between Orders
Aging Test, DIP Assembly and SMT Assembly: What the Line Maintains Between Orders
Most of what gets published about burn-in reliability is about proving things: curves, sample sizes, pass rates, the certificate a customer can file. Very little gets written about the hours when no customer lot is on the line at all. That gap is odd, because a reliability claim is only as good as the equipment that produced it, and equipment ages whether or not it is running paid work.
Between two orders, an aging test service line either keeps its assets honest or quietly lets them drift. The racks, the ovens, the solder pot on the wave side, the feeders up top — each of them wears in a different way, and none of them announces it. This piece walks through what a line that runs DIP assembly and SMT assembly actually services in the gaps between orders, and why those quiet hours decide what the next lot's data will say.
What the Aging Rack Does When Nothing Is Running
An empty aging rack is not an idle rack. Controllers hold their setpoints, data loggers keep polling, and the chamber cycles through its own standby routine. Maintenance here starts with observation: does the rack reach temperature at the same pace it did last quarter? A rack that has slowly begun to lag is telling you something about heaters, door seals or airflow long before it produces a failed lot. Walking the racks between orders, with a clipboard rather than a hurry, is the cheapest inspection a reliability operation can run.
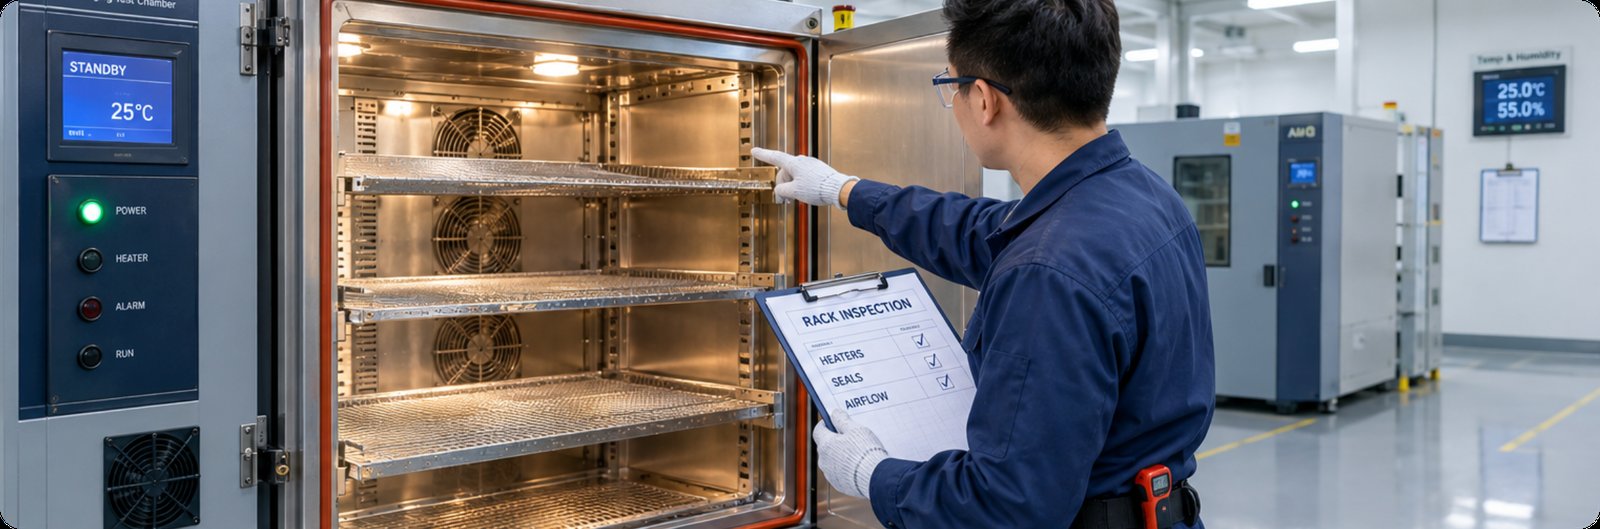
The second habit is power hygiene. Racks that sit switched off for days collect condensation in humid months, and contacts oxidize. A short powered warm-up before the next lot loads — long enough to chase moisture out of the chamber — costs almost nothing and removes a whole class of first-day failures that would otherwise be blamed on the boards.
The Oven Log Nobody Reads Until a Lot Fails
Every burn-in oven produces a log, and most logs live the same life: written faithfully, filed automatically, read never — until a customer lot comes back and somebody needs history in a hurry. The maintenance value of the log is not archival, it is diagnostic. A weekly skim of overlay traces will show a heater element losing margin, a fan bearing dragging, or a sensor that has started to agree less with its neighbours. None of those show up as a hard failure. They show up as a slow widening band on a chart that nobody has opened.
So the discipline is small: one person, one hour, one week, reading last week's traces against the month before. When the spread widens, service the hardware before the next manufacturing run commits to it. The lot that nearly failed is never the one that teaches you the most; the trace that drifted is.
Dummy Loads Keep the Soak Honest
An aging chamber that has only ever run full loads has never actually been tested at its rating. Dummy loads — resistive boards built to draw designed current and dissipate designed heat — are how a line verifies that a rack still does what its nameplate claims. They are also consumables nobody budgets for. Resistances drift, solder joints on load boards crack under thermal cycling, and a dummy load that has gone open on one channel turns a "full load" test into a partially loaded one without changing what the logger reports.
Between orders is exactly when to measure every load board, log its actual draw, and retire the ones that have wandered. It is unglamorous work with a direct payoff: when the next reliability report says "tested at full configured load", the sentence is true because somebody checked.
Solder Pot Care Between Waves
On the through-hole side, the asset that ages fastest is the one full of molten metal. A solder pot accumulates dross through every shift, and its alloy composition moves with every board that passes through — copper leaches upward, additives deplete, and the meniscus that wet beautifully in spring behaves differently by autumn. Between orders is when the pot gets skimmed properly rather than quickly, when a fresh ingot goes in to rebalance the bath, and when the impeller and nozzle that shape the wave get inspected for the erosion that slowly distorts it.
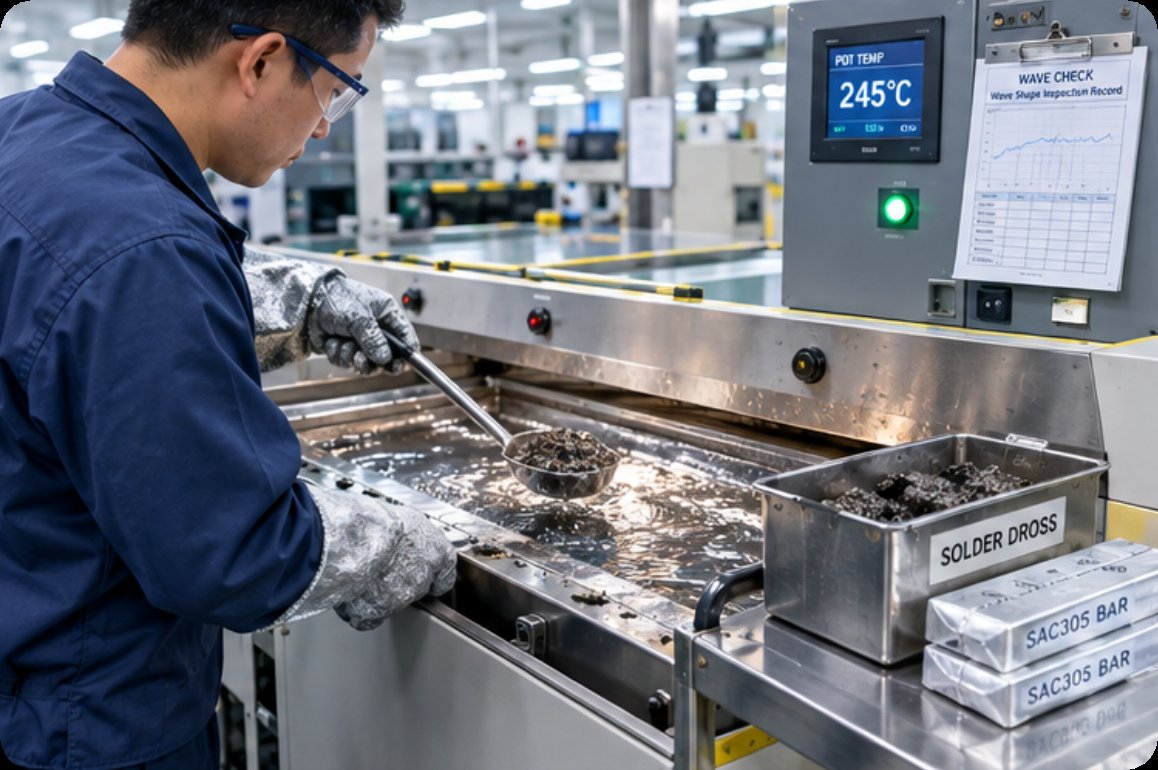
The tell that this work was skipped is subtle. Joints still form, boards still pass, but dross fines begin riding the wave onto leads, and touch-up hours quietly climb. A line that tracks its own touch-up time already knows what its pot maintenance schedule is worth.
Wear Items That Live on a Service Sheet
Placement equipment wears in small, countable ways. Nozzles pick up residue that quietly raises mis-pick rates. Feeders develop tape-advance slop that shows up first as occasional tombstones. Stencils accumulate tension loss and scratched apertures that print a little less past every hundred panels. None of these failures is dramatic, which is precisely why they belong on a printed service sheet rather than in anyone's memory. The sheet lists each wear item, its inspection interval, and the measurement that decides replace versus keep.
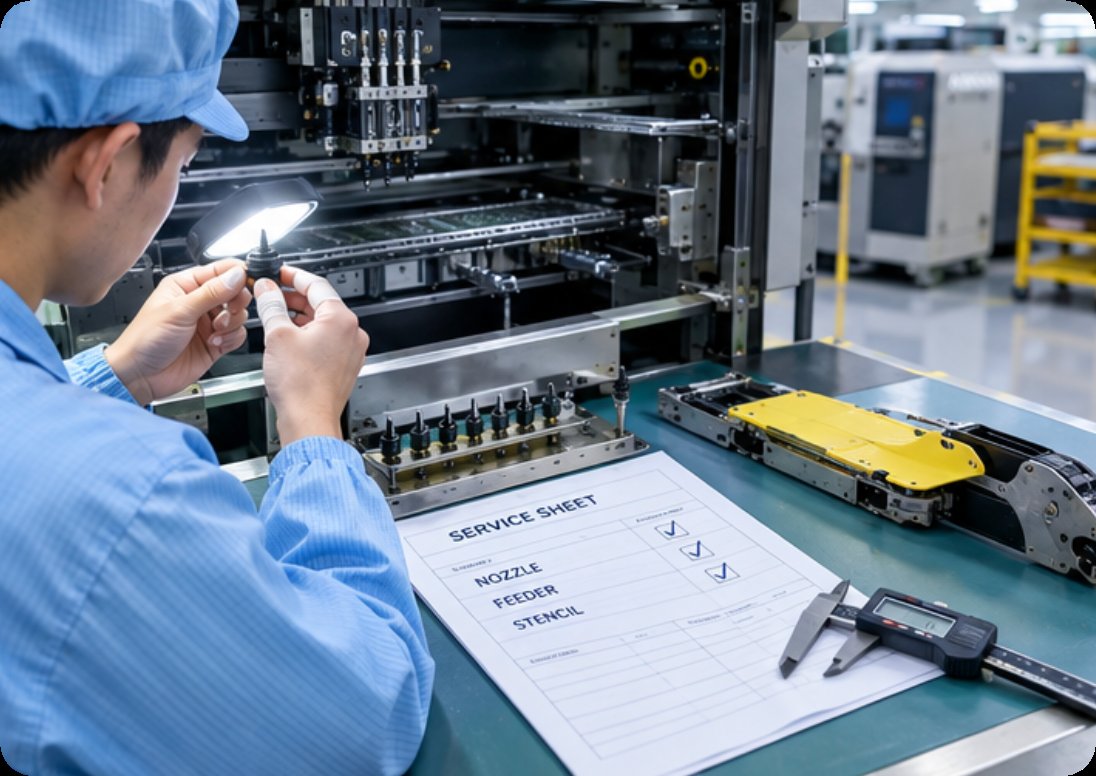
What makes the sheet work is that it is updated at the gap between orders, not during them. Stopping a running line to check a feeder is expensive; checking the same feeder while the line is dark costs a few minutes and a torch.
Cooldown Curves and What They Catch
One of the most underused maintenance signals in a burn-in operation is the cooldown. Every chamber cools on a characteristic curve, and that curve is effectively a fingerprint of its heaters, its fan and its seals working together. When cooling takes measurably longer than it did two quarters ago, something in that trio has degraded — usually before any high-temperature alarm has ever fired. Recording cooldown duration as a logged maintenance metric costs one column in a spreadsheet, and it catches heater and airflow decay earlier than any scheduled teardown.
One Sheet for Three Services
Because the aging, wave and placement sides wear differently, the useful artifact is a single cross-service table that says what gets checked, how, and what disqualifies the asset. Ours reads like this:
| Service | What wears out | Between-order check | Retire or service when |
|---|---|---|---|
| Aging Test | Heaters, door seals, logger probes, load boards | Trace skim, dummy-load draw measurement, powered warm-up | Cooldown lengthens or a load channel drifts open |
| DIP Assembly | Pot alloy balance, impeller, nozzle, dross tools | Full skim, ingot top-up, wave-shape inspection | Touch-up hours climb or the wave misshapes |
| SMT Assembly | Nozzles, feeders, stencil tension, apertures | Service-sheet walk with torch and gauge | Mis-pick or paste volume trend bends upward |
The table is deliberately qualitative. Exact intervals belong to the machine model and the duty cycle it sees; the constant is the habit — every wear item has a named check that happens when the line is empty, and a named measurement that ends the argument about whether it needs service.
Test Assets First, Rush Orders Second
There is a tempting accounting view in which hours without a customer lot are wasted capacity. The reliability view is the opposite: those hours are when the line earns the right to make claims. A burn-in result produced by a rack with drifting heaters and an unmeasured dummy load is not evidence; it is a rumour with a chart attached. The gap between orders is where the evidence gets manufactured, which makes the quiet hours part of the test rather than an interruption of it.
This is also where an electronics manufacturing services partner differs from a shop that only measures when it must. The habit of servicing assets between orders does not appear on any certificate, but it shows up in every lot's data afterwards — in tighter spreads, in fewer first-day chamber failures, in touch-up hours that stay flat all year. Buyers who walk a supplier floor between production runs can see the whole story in an afternoon: read the log shelf, ask when the load boards were last measured, look at the dross bin. The answers separate lines that maintain their assets from lines that merely own them.
If there is one ordering principle to take away, it is this: a line that lets test assets drift to win a week of throughput has borrowed against every future reliability claim it will make. The rack serviced between orders produces data that survives an audit. The one pushed straight from lot to lot produces whatever the log happens to say that week. Between orders is not downtime. For everything downstream that depends on trustworthy burn-in data, it is the most productive maintenance window the line has.
Tags: aging test / SMT assembly / DIP assembly / burn-in maintenance /
Prev: SMT Assembly and Industrial PC PCBA: The Evolution Written on a Witness Coupon
Next: PCB Fabrication, Aging Test and PCB Assembly: Following One Failed Board Home